
Supplier advantage is often presented as a mix of brochures, factory photographs, reference lists, and broad claims about quality, innovation, or global service. None of these is useless, but none is sufficient evidence for a technical purchasing decision. In power equipment, grid infrastructure, and industrial drive systems, the relevant question is narrower: can this supplier repeatedly deliver equipment that meets the stated duty, survives the operating environment, integrates into the project, and remains supportable over its service life?
An objective assessment therefore starts by converting supplier claims into verifiable requirements. “High reliability” becomes failure-rate evidence, design margins, test records, field-service data, and warranty conditions. “Fast delivery” becomes a documented production plan, critical-component lead times, inspection hold points, and logistics responsibility. “Strong engineering support” becomes named technical resources, response commitments, document quality, and a workable process for handling deviations.
The goal is not to identify a theoretically perfect supplier. It is to determine whether the supplier’s demonstrated capability matches the risk profile of the specific equipment package and project.
Define the duty before comparing suppliers
Technical comparisons become distorted when buyers request generic quotations for equipment that will face very different operating conditions. A medium-voltage switchgear lineup for a controlled industrial building is not equivalent to one installed in a humid coastal substation. A variable-frequency drive operating a clean-water pump has different harmonic, overload, cooling, and continuity requirements from a drive controlling a high-inertia conveyor or a critical process compressor.
Before evaluating supplier advantages, establish the conditions against which the advantage must be tested:
- Electrical duty: rated voltage, frequency, short-circuit level, insulation coordination, load profile, starting or overload duty, harmonic limits, and fault-clearing requirements.
- Environmental duty: ambient temperature range, altitude, humidity, salt mist, dust, vibration, corrosive gases, installation location, and enclosure constraints.
- System interfaces: upstream and downstream protection, SCADA or DCS protocol, existing relay platforms, cable arrangements, transformer impedance, earthing system, and cybersecurity requirements where digital connectivity is involved.
- Operational duty: permitted outage windows, maintainability expectations, spare-part strategy, local technical competence, and consequences of an unplanned shutdown.
- Commercial and contractual duty: delivery location, Incoterms, documentation language, inspection rights, liquidated-damages exposure, warranty start point, and acceptance definition.
This baseline prevents an attractive but incomplete offer from appearing equivalent to a more rigorously engineered proposal. A lower price may reflect a different enclosure rating, lower interrupting rating, excluded auxiliaries, reduced test scope, or an assumption that the buyer will resolve integration work on site. Comparing totals without reconciling these assumptions is not an objective assessment of supplier capability.
Request evidence that can be traced to the offered configuration
The most useful distinction is between general corporate evidence and evidence tied to the actual supply. A supplier may hold a relevant management-system certificate, have a well-equipped test facility, or manufacture a similar product family. These are positive indicators, but they do not automatically prove that the quoted equipment has the required performance.
For each critical requirement, ask for evidence at the appropriate level.
Standards require careful reading. Compliance with IEC, IEEE, UL, NEMA, or another recognized framework can be important, but a standard number alone does not settle the issue. Buyers need to identify the exact edition where relevant, the clauses applicable to the equipment, whether the evidence concerns a component or a completed assembly, and whether the tested arrangement matches the offered design.
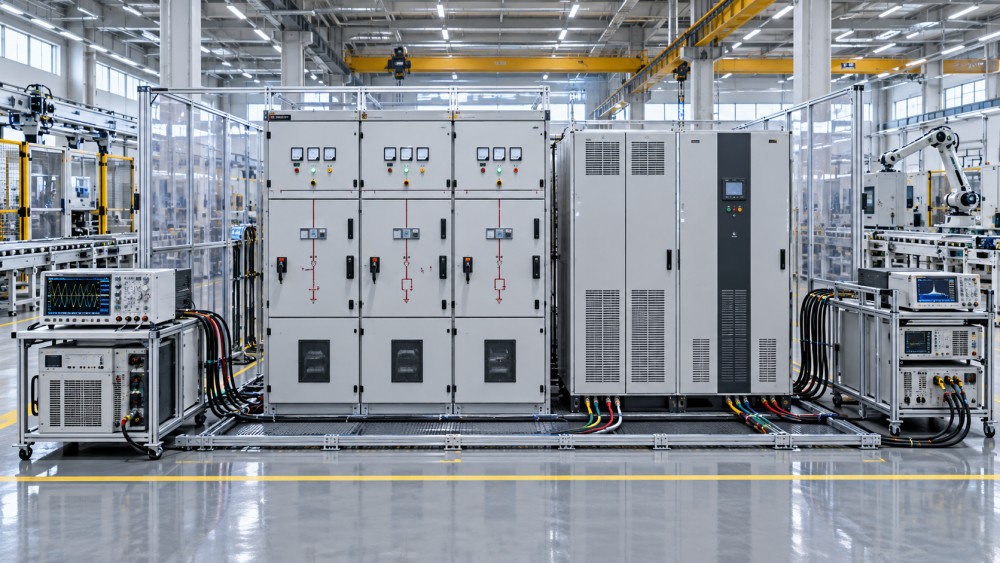
For example, a circuit breaker may have valid type-test evidence, while the complete switchgear assembly still requires separate consideration of internal arc classification, busbar arrangement, compartmentation, interlocking, and temperature rise. Likewise, a motor may meet an efficiency classification, yet the selected drive-motor-cable combination may still create insulation stress, bearing-current exposure, or cooling limitations at low speed. Supplier evaluation should follow the functional system boundary, not merely the most marketable component.
Separate type tests, routine tests, and project-specific verification
Test documentation is frequently treated as a binary pass-or-fail matter. It is more useful to distinguish what each test can actually establish.
Type tests demonstrate that a design, or a defined design family, can meet specified performance requirements under prescribed conditions. Their value depends on configuration relevance. A report for a different frame size, enclosure, busbar layout, interrupting device, or insulation system may support an engineering argument, but it is not identical proof.
Routine tests confirm that the supplied unit has been manufactured and checked according to the applicable production requirements. Typical examples may include wiring checks, dielectric tests, functional checks, calibration verification, and mechanical operation tests, depending on equipment type. Routine testing cannot replace type testing, but it is essential because even a qualified design can be incorrectly assembled or configured.
Factory acceptance testing should focus on the actual project risks. A generic FAT checklist is often too shallow for integrated packages. For protection and control panels, this may require checking logic narratives, trip matrices, communication points, time synchronization, alarms, interlocks, and simulated inputs. For a drive system, it may require confirming parameter sets, interface signals, cooling provisions, bypass logic, and fault behavior. For packaged substations or switchgear, the FAT should reconcile nameplates, drawings, wiring, protection settings, and customer-specific accessories against the approved documentation.
Where witness testing is impractical, a buyer can still require dated test records, photographs of identification plates and test setups, calibrated-instrument references, signed deviation logs, and a clear release process. The principle is simple: acceptance evidence should be sufficiently detailed that an independent reviewer can understand what was tested, under which conditions, and what exceptions remain.
Evaluate engineering discipline, not only engineering capacity
Supplier brochures often emphasize the size of an engineering team. Team size says little about whether the supplier can control interfaces and changes. The more revealing question is how engineering decisions are documented and governed.
A capable supplier should be able to provide a coherent document chain: datasheets, general arrangement drawings, single-line diagrams, schematics, terminal plans, cable schedules, bill of materials, protection studies or setting assumptions where included, communication architecture, and operation-and-maintenance instructions. These documents should agree with one another. Inconsistent tag numbers, unexplained rating changes, missing terminal details, or unclear revision history are not administrative inconveniences. They are early warnings of integration and commissioning risk.
Design review is particularly important where equipment interacts with an existing grid or plant. A supplier advantage may lie in identifying issues before manufacture: insufficient fault rating at the point of connection, incompatible control voltage, unavailable panel space, protection coordination gaps, transformer inrush effects, harmonic resonance, or an unsupported communication topology. The ability to raise these matters constructively is more valuable than simply accepting every line in a purchase specification.
That does not mean suppliers should be allowed to change requirements informally. A disciplined deviation process is needed. Every proposed deviation should state the original requirement, the proposed alternative, technical consequences, commercial consequences, affected documents, and the approval needed. “Equivalent” is not an engineering conclusion unless equivalence is demonstrated against the application conditions.
Assess reliability through lifecycle mechanisms
Reliability claims are difficult to compare because field conditions vary and public failure data are rarely normalized across suppliers. Rather than demanding a single reliability percentage, examine the mechanisms that influence lifecycle performance.
For electrical equipment, these mechanisms can include component sourcing and obsolescence control, thermal margin, creepage and clearance design, insulation system selection, enclosure sealing, coating quality, busbar joint design, cooling path maintenance, relay firmware management, and spare-part availability. For rotating equipment and drives, attention may also be needed on bearing arrangements, inverter duty, cooling at reduced speed, vibration exposure, cable length, output filtering, and service access.
The supplier should be able to explain how critical components are qualified, what happens when an approved component becomes unavailable, and whether substitutions require customer approval. This is especially relevant in a supply environment where electronic components, semiconductors, relays, communication modules, and specialized materials may be subject to long lead times or redesign cycles. A technically sound original design can become a project risk if substitutions are managed only through purchasing rather than formal engineering control.
Warranty wording also deserves closer inspection. A long warranty period has limited value if exclusions are broad, failure diagnosis is undefined, labor and travel are excluded, or replacement lead time is not addressed. The practical question is not merely who owns the defective part; it is who bears the operational consequence while the issue is being investigated and corrected.
Test delivery capability using the critical path
Delivery performance should be assessed as an operating system, not as a date stated in a quotation. Request a milestone schedule from engineering release through procurement, fabrication, assembly, testing, packing, shipment, and document handover. Then identify the activities that can actually delay the project.
Critical path items differ by equipment. They may include vacuum interrupters, copper or aluminum conductors, transformers, power semiconductors, specialized protection relays, cast-resin components, enclosures, or customer-approved drawings. A supplier that claims a short lead time should be able to show whether these items are in stock, reserved under framework arrangements, already ordered, or still subject to quotation.
Production capacity must also be interpreted correctly. A large factory does not guarantee availability for a particular order. Useful evidence includes current production loading, line allocation, subcontracted-process control, manufacturing records for comparable equipment, and the capacity to perform required testing without delaying shipment. For cross-border supply, export packing, dangerous-goods obligations where applicable, customs documentation, origin documentation, and destination-specific labeling can be as consequential as the manufacturing schedule.
Objectivity requires treating schedule confidence separately from stated lead time. A longer but documented schedule may present less risk than an aggressive date unsupported by material status or approved drawings.
Measure support by response architecture
Engineering support becomes visible when something does not go as planned: a site dimension differs from the drawing, a protection signal is missing, an insulation test raises concern, a communication link fails, or a component must be replaced under time pressure. The relevant supplier advantage is not the promise of “24/7 support,” but the architecture behind it.
Clarify who owns technical questions before shipment, during commissioning, and after handover. Confirm whether support is provided directly by the design authority or filtered through a sales channel. Establish escalation contacts, expected response windows, remote-access constraints, language capability, availability of commissioning personnel, and responsibility for revised drawings or firmware files.
For digitally connected equipment, support scope must include configuration management. The buyer should know which firmware versions are supplied, how parameter backups are stored, who can alter settings, what access credentials are transferred, and how compatibility is preserved when devices are replaced. A system that functions at FAT but cannot be securely maintained after commissioning does not offer durable operational value.
Use a weighted decision record, but do not hide uncertainty inside a score
A scoring model can improve discipline if it is built around project-critical conditions. It can also create false confidence when subjective impressions are converted into precise-looking numbers. The best use of a scorecard is to expose trade-offs and evidence gaps.
Weight criteria according to the consequence of failure. In a critical grid connection, verified short-circuit performance, protection integration, manufacturing control, and service response may deserve greater emphasis than small differences in purchase price. In a standardized, non-critical auxiliary application, interchangeability, availability, and landed cost may reasonably carry more weight.
Each score should include a written evidence reference: document number, revision, test report, meeting record, approved deviation, or contractual commitment. A score without traceable support is only an opinion. It is also useful to distinguish between “evidence confirms compliance,” “evidence suggests compliance but needs clarification,” and “requirement is not met.” This prevents a supplier with unresolved technical gaps from being treated as nearly equal merely because the spreadsheet average remains high.
The final decision should retain an exception register. It should identify open technical deviations, missing documents, unproven interfaces, commercial assumptions, and mitigation owners. Procurement risk is often created not by the issues known during evaluation, but by issues that were noticed, discussed, and never formally closed.
What an objective conclusion looks like
A defensible supplier assessment does not declare one company universally superior. It reaches a more useful conclusion: this supplier is suitable, conditionally suitable, or unsuitable for this defined scope under these operating and contractual conditions.
The supplier with the strongest advantage is not necessarily the one with the most polished presentation, the lowest quotation, or the longest catalog of certifications. It is the one whose offered configuration can be traced from requirement to design evidence, manufacturing controls, test records, delivery plan, interface responsibility, and lifecycle support. When those links are visible, supplier selection becomes an engineering and commercial judgment grounded in evidence rather than a contest between marketing claims.
Related News
- How Can Technical Buyers Assess Supplier Advantages Objectively?Sep 28, 2026How can I assess supplier advantages without relying on marketing claims? Use traceable tests, lifecycle risk checks, delivery evidence, and support metrics.
- Evaluating Steam Turbine Suppliers for Captive Power Plant ProjectsSep 28, 2026Steam turbine supplier evaluation for captive power plants: compare steam balance fit, guarantees, quality controls, delivery risk, and lifecycle support before selecting a partner.
- How to verify suppliers listed in a power system supplier directorySep 19, 2026Power system supplier directory verification guide: validate legal identity, technical compliance, factory quality, delivery capacity, references, and risk before selecting electrical equipment partners.
- What to verify before choosing an energy storage system supplierSep 17, 2026Energy storage system supplier checklist: verify system fit, certifications, safety, warranty, delivery capacity, and service support before committing to a contract.
Related News
- 00
0000-00
How smart switchgear condition monitoring detects early faults - 00
0000-00
How industrial infrastructure development can reduce project delivery risk - 00
0000-00
How to size power equipment for factories without overbuilding capacity - 00
0000-00
How efficiency evolution in automation is reshaping factory energy use - 00
0000-00
When market scanning services are worth the investment